 by
Page Contents
Introduction
A concrete mix may be calculated correctly and still behave differently during a laboratory trial, batching-plant trial or actual site production.
Common problems include:
- slump lower than expected;
- excessive slump;
- rapid slump loss;
- harsh concrete;
- sticky concrete;
- segregation;
- excessive bleeding;
- poor pumpability;
- abnormal fresh-concrete density;
- incorrect concrete yield;
- rapid or delayed setting;
- low early strength;
- low 28-day strength;
- excessive variation in strength.
The correct response is not to change several ingredients at the same time.
A systematic troubleshooting process should be followed:
Observe the Problem → Verify Measurements → Identify the Likely Cause → Make One Controlled Adjustment → Repeat the Trial → Compare Results → Approve the Correction
Concrete troubleshooting is therefore different from basic mix-design calculation.
The purpose of troubleshooting is to identify why a concrete mix is not performing as expected and correct the problem without unnecessarily changing water, cement or other ingredients.
For the complete concrete mix-design sequence, visit the Concrete Mix Design Hub.
Why Can a Correct Concrete Mix Design Still Have Problems?
Concrete mix design is based on:
- measured material properties;
- assumed moisture conditions;
- specified workability;
- selected admixture dosage;
- laboratory trial results.
Actual production conditions may be different.
Performance can change because of:
- aggregate moisture variation;
- aggregate grading variation;
- cement properties;
- concrete temperature;
- admixture performance;
- batching accuracy;
- mixing sequence;
- mixing time;
- transportation time;
- pumping;
- sampling and testing errors.
Therefore:
Mix calculation provides the starting proportions. Trial mixes and production control confirm the final workable proportions.
First Rule of Concrete Mix Troubleshooting
Before changing the concrete mix, confirm that the observed problem is genuine.
Check:
- correct mix-design ID;
- correct mix revision;
- correct material quantities;
- aggregate moisture;
- testing procedure;
- concrete sampling;
- concrete temperature;
- time after mixing;
- weighing system;
- batching-plant calibration.
Sometimes an apparent mix-design problem is actually a:
- batching problem;
- moisture problem;
- testing problem;
- equipment problem.
Recommended Troubleshooting Sequence
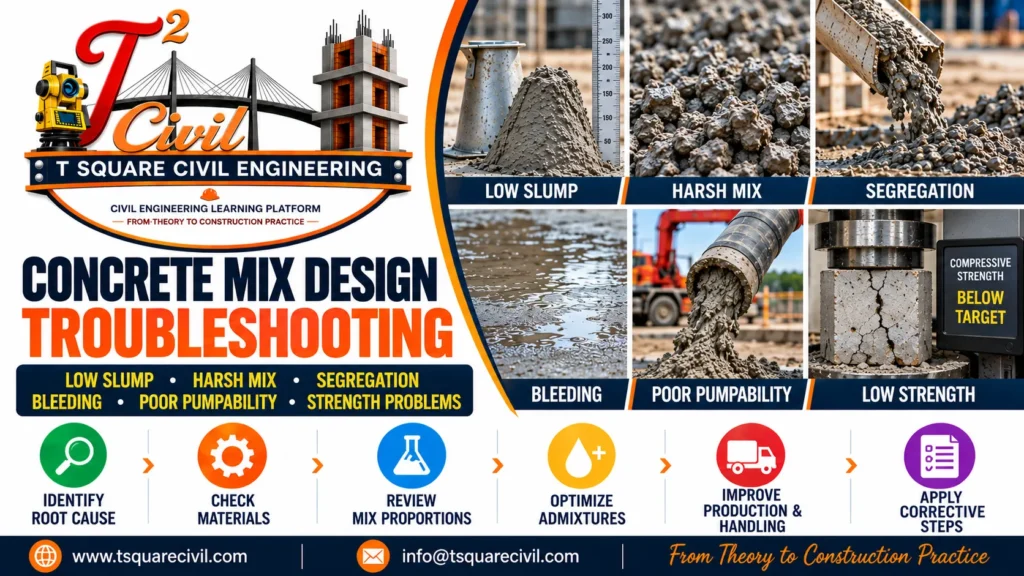
Follow this sequence whenever possible:
Verify Test Result
↓
Check Batch Quantities
↓
Check Aggregate Moisture
↓
Check Concrete Temperature and Elapsed Time
↓
Check Aggregate Grading
↓
Check Admixture Dosage
↓
Check Cement–Admixture Compatibility
↓
Review Paste and Aggregate Proportions
↓
Change Only the Necessary Variable
↓
Repeat the Trial and Record the Result
This approach helps prevent uncontrolled trial-and-error adjustments.
Problem 1 – Concrete Slump Is Lower Than Required
Suppose the required slump is:
150 mm
but the actual slump is:
80 mm
Do not immediately add water.
Low slump can result from several causes.
Incorrect Aggregate Moisture Correction
If the fine aggregate is drier than assumed, it may absorb part of the mixing water.
The concrete then behaves as if less effective water were available.
Check actual aggregate moisture before changing the mix.
For detailed calculations, see Moisture Correction in Concrete Mix Design.
High Concrete Temperature
High concrete temperature can increase:
- rate of hydration;
- evaporation;
- slump loss.
A concrete mix that performs well in cooler conditions may become less workable in hot weather.
Insufficient Superplasticizer
If the HRWRA or superplasticizer dosage is too low, the required workability may not be achieved.
However, the dosage should be adjusted through trials and within the approved dosage range.
Cement–Admixture Compatibility Problem
Some cement and admixture combinations may show:
- poor initial dispersion;
- rapid slump loss;
- unexpected setting behaviour.
See Cement–Admixture Compatibility in Concrete Mix Design.
Fine Aggregate Is Too Fine
Very fine sand has a higher surface area.
This may increase:
- water demand;
- paste demand;
- admixture demand.
Excess Fine Aggregate
Too much fine aggregate can increase internal friction and make the concrete difficult to move.
Angular Aggregate
Highly angular crushed aggregate or M-sand may require more:
- paste;
- lubrication;
- admixture.
See Manufactured Sand (M-Sand) in Concrete Mix Design.
Corrective Approach for Low Slump
Use this sequence:
Check Moisture → Check Temperature → Check Batch Record → Check Admixture → Check Grading → Review Sand Content → Repeat Trial
Do not change the design water until the root cause has been identified.
Problem 2 – Concrete Slump Is Higher Than Required
Suppose the required slump is:
100–125 mm
but the measured slump is:
190 mm
Possible causes include:
- excess batch water;
- wet aggregate not properly corrected;
- excessive admixture dosage;
- incorrect water-meter calibration;
- wrong mix selected;
- incorrect batching.
Example – Effect of Unaccounted Surface Moisture
Suppose:
Design free water = 160 kg/m³
Unaccounted water from wet aggregate = 15 kg/m³
Actual free water becomes:
160 + 15 = 175 kg/m³
If cementitious material is:
400 kg/m³
Design w/cm:
160 ÷ 400 = 0.40
Actual w/cm:
175 ÷ 400 = 0.438
This is a significant change.
Corrective Approach
Check:
- aggregate moisture;
- batch water;
- admixture dosage;
- plant records;
- calibration.
Do not try to correct an excessively wet batch by randomly adding cement or aggregate.
See Concrete Batching Plant Calibration.
Problem 3 – Rapid Slump Loss
Concrete may initially meet the required slump but lose workability quickly.
Example:
| Time | Slump |
|---|---|
| Initial | 180 mm |
| 30 minutes | 140 mm |
| 60 minutes | 85 mm |
| 90 minutes | 40 mm |
Rapid slump loss can create serious problems in:
- ready-mixed concrete;
- pumped concrete;
- congested reinforcement;
- long-distance transportation.
Possible Causes
- high concrete temperature;
- high cement temperature;
- cement–admixture incompatibility;
- insufficient slump-retaining admixture;
- excessive fines;
- absorptive aggregate;
- long transport time;
- unsuitable mixing sequence.
Corrective Approach
Possible corrective actions include:
- control concrete temperature;
- optimize the admixture system;
- review admixture addition sequence;
- account correctly for aggregate absorption;
- review fine-particle content;
- conduct timed slump-retention trials.
Do not automatically increase the initial mixing water.
A dedicated article on Slump Loss in Concrete will cover this topic in greater detail.
Problem 4 – Concrete Is Harsh
Harsh concrete is difficult to:
- place;
- compact;
- pump;
- finish.
It may appear coarse and have insufficient mortar around the aggregate.
Signs of Harsh Concrete
- visible coarse aggregate;
- poor cohesion;
- difficult finishing;
- poor pumpability;
- high internal friction;
- aggregate separation.
Possible Causes
Excess Coarse Aggregate
Too much coarse aggregate reduces the mortar available to surround and lubricate particles.
Insufficient Fine Aggregate
Too little sand can produce an open and coarse concrete texture.
Poor Aggregate Grading
Gap grading can reduce packing efficiency.
Insufficient Paste
Low paste volume may produce harsh concrete even when w/cm is correct.
Highly Angular Aggregate
Angular aggregate increases internal friction.
Corrective Approach
Possible adjustments include:
- slightly increasing fine aggregate proportion;
- reducing excessive coarse aggregate;
- improving combined grading;
- reviewing paste volume;
- optimizing admixture dosage.
Any adjustment should be verified by trial mix.
See Fine and Coarse Aggregate Proportioning in Concrete Mix Design.
Problem 5 – Concrete Is Too Sticky
Sticky concrete is different from properly cohesive concrete.
A good concrete mix should be cohesive.
However, excessive stickiness can make concrete:
- difficult to discharge;
- difficult to pump;
- difficult to compact;
- difficult to finish.
Possible Causes
- excessive fine aggregate;
- excessive fines;
- excessive powder;
- high paste viscosity;
- excessive VMA;
- very low w/cm;
- poor aggregate balance.
M-sand and high-powder mixes may be particularly sensitive.
Corrective Approach
Check:
- sand grading;
- sand percentage;
- material finer than 150 µm;
- total powder content;
- coarse aggregate proportion;
- HRWRA dosage;
- VMA dosage where used.
Do not simply add water to reduce stickiness.
Problem 6 – Concrete Segregates
Segregation occurs when the components of concrete separate and the mixture no longer remains uniform.
Typical signs include:
- coarse aggregate separating from mortar;
- mortar flowing ahead of aggregate;
- stones collecting at the bottom;
- highly fluid concrete with poor stability.
Common Causes
Excess Water
Too much water reduces cohesion.
Excessive Workability
Very high flow without sufficient stability may cause separation.
Insufficient Fine Material
The mortar phase may not be able to support coarse aggregate.
Excess Coarse Aggregate
Too much coarse aggregate may reduce stability.
Excessive Superplasticizer
Overdosing may produce high flow with inadequate stability.
Poor Aggregate Grading
Large gaps in grading may increase segregation risk.
Poor Placement Practice
Even a good mix may segregate if:
- dropped from excessive height;
- over-vibrated;
- handled improperly.
Corrective Approach
Check:
Water → Admixture → Sand Content → Fines → Aggregate Grading → Coarse Aggregate Quantity → Placement Method
For SCC, segregation resistance should be checked together with flow and passing ability.
See Self-Compacting Concrete Mix Design.
Problem 7 – Excessive Bleeding
Bleeding occurs when water moves upward through fresh concrete while solid particles settle.
Excessive bleeding may cause:
- weak surface concrete;
- laitance;
- poor bond;
- settlement around reinforcement;
- finishing problems.
Possible Causes
- excessive water;
- insufficient fines;
- low cementitious content;
- poor aggregate grading;
- excessive coarse aggregate;
- delayed setting;
- unsuitable admixture behaviour.
Corrective Approach
Review:
- free-water content;
- w/cm;
- sand grading;
- fine-particle content;
- paste content;
- SCM system;
- admixture effect;
- setting behaviour.
Do not automatically increase cement content without identifying the actual cause.
Problem 8 – Concrete Has Little Bleeding but Is Very Sticky
Little or no visible bleeding does not automatically mean that the concrete is ideal.
A very fine or powder-rich mix may show:
- little bleeding;
- high viscosity;
- excessive stickiness;
- difficult finishing;
- increased pumping pressure.
The desired condition is:
Workable + Cohesive + Stable
not simply:
No Bleeding
Problem 9 – Poor Pumpability
Concrete can have an acceptable slump and still pump poorly.
Therefore:
Slump does not automatically indicate pumpability.
Pumpable concrete requires:
- suitable mortar volume;
- continuous grading;
- adequate fines;
- stable workability;
- suitable aggregate size;
- sufficient pipeline lubrication.
Symptoms of Poor Pumpability
- high pump pressure;
- pressure fluctuation;
- pipeline blockage;
- irregular concrete flow;
- segregation;
- mortar-only discharge;
- rapid slump loss.
Possible Causes
- insufficient mortar;
- poor aggregate grading;
- excessive coarse aggregate;
- highly angular aggregate;
- insufficient fines;
- excessive fines causing stickiness;
- inadequate slump retention.
See Pumped Concrete Mix Design.
Problem 10 – Fresh Concrete Density Is Lower Than Expected
Suppose expected fresh density is approximately:
2400 kg/m³
but measured density is:
2280 kg/m³
Possible causes include:
- excessive air;
- incorrect aggregate quantity;
- wrong assumed specific gravity;
- batching error;
- segregation;
- incorrect test procedure.
Verify the test and batch record before changing the mix.
See Fresh Concrete Density and Yield in Concrete Mix Design.
Problem 11 – Fresh Concrete Density Is Higher Than Expected
Possible causes include:
- excessive aggregate quantity;
- lower-than-expected air content;
- incorrect yield;
- material specific gravity different from design;
- weighing error.
Fresh density should always be reviewed together with batch yield and batch records.
Problem 12 – Concrete Yield Is Lower Than Expected
Suppose materials were batched for:
6.0 m³
but the actual yield appears significantly lower.
Possible causes include:
- incorrect material specific gravity;
- incorrect batching;
- aggregate moisture error;
- incorrect assumed air content;
- weighing-system error;
- calculation error.
Do not compensate by simply increasing all batch quantities.
The cause of the volume difference should first be identified.
Problem 13 – Concrete Sets Too Quickly
Rapid setting may cause:
- finishing problems;
- cold joints;
- pumping difficulty;
- rapid workability loss.
Possible Causes
- high concrete temperature;
- high cement temperature;
- cement characteristics;
- unsuitable admixture;
- incorrect admixture dosage;
- long transportation;
- incompatible cement–admixture combination.
Corrective Approach
Check:
- cement source;
- material temperature;
- concrete temperature;
- admixture;
- transport duration;
- mixing sequence.
Problem 14 – Concrete Sets Too Slowly
Delayed setting may affect:
- formwork cycle;
- finishing;
- construction sequence;
- early strength.
Possible causes include:
- excessive retarding admixture;
- low temperature;
- high SCM replacement;
- cement–admixture interaction;
- excessive admixture dosage.
Slow setting does not automatically mean low final strength.
The later-age concrete strength should still be evaluated.
Problem 15 – Low 7-Day Strength
Low 7-day strength does not always mean that 28-day strength will fail.
Possible reasons include:
- high SCM replacement;
- low curing temperature;
- slower binder reaction;
- specimen curing error;
- testing error;
- excessive actual w/cm;
- batching error.
Check Before Changing the Mix
Verify:
- cube identification;
- sampling;
- compaction;
- curing;
- test machine;
- water quantity;
- cementitious quantity;
- batch records.
See Concrete Cube Casting Procedure.
Problem 16 – Low 28-Day Strength
Low 28-day strength requires systematic investigation.
Possible Causes
Excessive Actual w/cm
Possible reasons:
- excess batch water;
- unaccounted aggregate moisture;
- site water addition.
Insufficient Cementitious Material
Possible reasons:
- weighing error;
- wrong mix selection;
- batching-system problem.
Material Variation
Changes in:
- cement;
- SCM;
- aggregate;
- admixture
may change strength.
Cube Preparation or Testing Error
Low test results can also result from:
- poor sampling;
- insufficient compaction;
- damaged specimens;
- incorrect curing;
- improper testing.
Poor Site Concrete
Structural concrete may also be affected by:
- poor compaction;
- segregation;
- inadequate curing.
Therefore, determine whether the problem comes from:
Mix Design
Production
Testing
or:
Site Placement and Curing
before changing the concrete proportions.
Problem 17 – Concrete Strength Is Much Higher Than Required
Very high strength may seem beneficial, but it can indicate an unnecessarily rich mix.
Example:
Required grade:
M30
Average production strength:
55 MPa
This may indicate:
- excessive cementitious content;
- unnecessarily low w/cm;
- overly conservative assumptions.
Excessive overdesign may increase:
- cost;
- heat of hydration;
- shrinkage;
- environmental impact.
The mix should maintain the required statistical margin without unnecessary overdesign.
Problem 18 – Large Variation in Cube Strength
Suppose 28-day strengths are:
32 MPa
46 MPa
35 MPa
48 MPa
Such variation may indicate weak production control even if the average appears satisfactory.
Possible causes include:
- varying batch water;
- changing aggregate moisture;
- cement variation;
- aggregate variation;
- inconsistent admixture dosing;
- poor batching;
- sampling variation;
- curing variation;
- testing variation.
The problem is not simply average strength.
The real issue may be high variability.
See Target Mean Strength of Concrete.
Problem 19 – Strength Gradually Reduces Over Time
A gradual downward strength trend is different from one isolated low result.
Check whether anything changed in:
- cement source;
- cement lot;
- sand source;
- quarry source;
- sand grading;
- M-sand fines;
- aggregate moisture;
- SCM;
- admixture;
- batching calibration;
- curing;
- laboratory testing.
Strength trends can identify production deterioration before a major failure occurs.
See Concrete Mix Design Approval and Production Control.
Problem 20 – Excess Mortar Appears at the Surface
Possible causes include:
- excessive fine aggregate;
- excessive paste;
- segregation;
- over-vibration;
- excessive workability.
Check whether coarse aggregate is settling while mortar rises.
Do not judge the problem from surface appearance alone.
Problem 21 – Coarse Aggregate Accumulates at the Bottom
Possible causes include:
- segregation;
- excessive water;
- very high slump;
- insufficient viscosity;
- excessive vibration.
In SCC, this may indicate inadequate segregation resistance.
Problem 22 – Concrete Is Difficult to Finish
Possible causes include:
- harsh grading;
- insufficient mortar;
- highly angular aggregate;
- insufficient paste;
- excessive stickiness;
- excessive fines;
- rapid slump loss.
First determine whether the concrete is:
Too Harsh
or:
Too Sticky
These are different problems and require different corrections.
Problem 23 – Surface Laitance Develops
Laitance is a weak surface layer containing fine cementitious material and water.
Possible causes include:
- excessive bleeding;
- excess water;
- overworking the surface;
- finishing while bleed water is present.
This may be partly a site finishing problem rather than a mix-design problem.
Problem 24 – Laboratory Trial Is Good but Site Concrete Is Poor
This is a common production issue.
Laboratory concrete may have:
- carefully controlled moisture;
- precise weighing;
- stable temperature;
- short handling time.
Production concrete may experience:
- changing moisture;
- large batch quantities;
- transport delay;
- high temperature;
- pumping;
- batching errors;
- site water addition.
Therefore, if laboratory concrete is satisfactory but site concrete is poor, investigate:
production conditions before redesigning the mix.
Problem 25 – Concrete Worked Yesterday but Not Today
Do not assume the mix design suddenly became incorrect.
Ask what changed.
Check:
- Did it rain?
- Did sand moisture change?
- Did the cement tanker change?
- Did the aggregate source change?
- Did temperature increase?
- Was a new admixture batch introduced?
- Did transport time increase?
- Was the batching plant repaired?
- Was a moisture sensor changed?
Concrete troubleshooting often begins by identifying what changed between the good batch and the bad batch.
Change Only One Main Variable at a Time
This is one of the most important troubleshooting principles.
Suppose the mix is harsh.
Do not simultaneously:
- increase water;
- increase sand;
- increase admixture;
- reduce coarse aggregate;
- increase cement.
If the next trial improves, you will not know which change solved the problem.
Instead:
Trial 1 → Identify Problem
↓
Trial 2 → Make One Main Adjustment
↓
Compare Results
↓
Trial 3 → Fine-Tune if Required
This creates useful technical evidence.
Keep Workability Control Separate From w/cm
Another important rule is:
Workability should not be controlled by uncontrolled changes in w/cm.
Workability can often be improved using:
- aggregate grading;
- aggregate proportion;
- moisture control;
- suitable HRWRA;
- paste optimization.
Increasing free water should not be the default solution.
Concrete Troubleshooting Matrix
| Observed Problem | Check First | Possible Adjustment |
|---|---|---|
| Low slump | Moisture, temperature, admixture | Optimize HRWRA / grading |
| High slump | Water, wet aggregate, admixture | Correct dosing |
| Rapid slump loss | Temperature, compatibility | Improve retention |
| Harsh mix | Sand %, grading, paste | Improve mortar balance |
| Sticky mix | Fines, powder, sand | Reduce excessive viscosity |
| Segregation | Water, flow, coarse aggregate | Improve stability |
| Bleeding | Water, fines, paste | Optimize water and fines |
| Poor pumpability | Grading, mortar, retention | Improve pumpable matrix |
| Low density | Air, batching, SG | Verify material and batching |
| Low strength | w/cm, batching, curing | Identify root cause |
| Excessive strength | Binder, w/cm | Review economy |
| Variable strength | Moisture, batching, testing | Strengthen QC |
Root-Cause Troubleshooting Table
| Problem | Possible Material Cause | Possible Production Cause |
|---|---|---|
| Low slump | Fine sand, angular aggregate | Dry aggregate, low admixture |
| High slump | — | Excess water, wet sand |
| Slump loss | Cement/admixture interaction | Heat or transport delay |
| Segregation | Poor grading | Excess water, handling |
| Bleeding | Insufficient fines | Excess water |
| Low strength | High w/cm or poor material | Batching or curing error |
| Variable strength | Material variability | Moisture / weighing variation |
| Low yield | Incorrect specific gravity | Batch quantity error |
Trial Adjustment Record
Every trial adjustment should be documented.
| Parameter | Trial 1 | Trial 2 | Trial 3 |
|---|---|---|---|
| Cementitious Material | ___ | ___ | ___ |
| Water | ___ | ___ | ___ |
| w/cm | ___ | ___ | ___ |
| Fine Aggregate | ___ | ___ | ___ |
| Coarse Aggregate | ___ | ___ | ___ |
| Admixture | ___ | ___ | ___ |
| Initial Slump | ___ | ___ | ___ |
| 30-Minute Slump | ___ | ___ | ___ |
| Fresh Density | ___ | ___ | ___ |
| Segregation | ___ | ___ | ___ |
| Bleeding | ___ | ___ | ___ |
| 7-Day Strength | ___ | ___ | ___ |
| 28-Day Strength | ___ | ___ | ___ |
| Remarks | ___ | ___ | ___ |
Always record:
What Was Changed + Why It Was Changed + What Happened
Example – Correcting a Harsh Trial Mix
Suppose Trial 1 gives:
Slump:
110 mm
Segregation:
None
Concrete appearance:
Harsh with excessive visible coarse aggregate
Do not immediately increase water.
Check the aggregate balance.
Suppose the fine aggregate fraction is relatively low.
For Trial 2, make a controlled adjustment:
Increase Fine Aggregate Slightly
and:
Reduce Corresponding Coarse Aggregate Volume
while maintaining:
- total aggregate volume;
- free-water content;
- w/cm;
- cementitious content.
Then compare:
- workability;
- cohesion;
- density;
- strength.
This helps determine whether aggregate proportion caused the harshness.
Example – Correcting Excessive Slump
Suppose:
Target slump:
150 ± 25 mm
Actual slump:
220 mm
Before reducing admixture, check:
- sand moisture;
- batch-water record;
- any site water addition.
Suppose unaccounted free water from sand is:
12 kg/m³
The correct action is:
Correct Aggregate Moisture and Reduce Separately Added Water
not automatically:
Reduce Superplasticizer
This is why root-cause diagnosis is important.
Example – Slump Is Correct but Strength Is Low
Suppose:
Slump:
150 mm
28-day strength:
Below Target
Do not immediately increase cement.
Check:
- actual w/cm;
- aggregate moisture;
- site water addition;
- cementitious batching;
- plant calibration;
- cube preparation;
- curing;
- testing.
A concrete mix can have acceptable slump even when actual water content is too high.
Laboratory Trial vs Production Problem
A simple troubleshooting rule is:
If Both Laboratory and Plant Concrete Show the Same Problem
Investigate:
mix proportions and material properties
If Laboratory Concrete Is Good but Plant Concrete Is Poor
Investigate:
batching, moisture, temperature, mixing, transport and production control
This can avoid unnecessary redesign.
When Should the Concrete Mix Design Be Revised?
A permanent mix-design revision may be required when a significant change occurs in:
- cement source;
- aggregate source;
- aggregate grading;
- SCM;
- admixture;
- concrete grade;
- workability requirement;
- placement method.
Normal day-to-day aggregate moisture correction does not automatically require a new mix-design revision.
See Concrete Mix Design Approval and Production Control.
When Should the Batching Plant Be Investigated?
Check the batching plant when you observe:
- sudden variation after stable production;
- unexplained water variation;
- repeated under-batching;
- repeated over-batching;
- abnormal yield;
- unusual material consumption;
- admixture dosing variation;
- unexplained strength variation.
See Concrete Batching Plant Calibration.
Troubleshooting High-Strength Concrete
High-strength concrete is especially sensitive to:
- small water variations;
- aggregate moisture;
- HRWRA dosage;
- concrete temperature;
- cementitious compatibility.
Even a small unaccounted increase in water can significantly affect a low-w/cm mix.
See High-Strength Concrete Mix Design.
Troubleshooting Self-Compacting Concrete
SCC should not be evaluated only from slump flow.
Check:
- filling ability;
- T500;
- passing ability;
- viscosity;
- segregation resistance.
A large slump-flow diameter is not desirable if the concrete segregates.
See Self-Compacting Concrete Mix Design.
Troubleshooting M-Sand Concrete
For M-sand concrete, common problems may result from:
- excessive fines;
- crusher grading variation;
- angular particle shape;
- moisture variation.
See Manufactured Sand (M-Sand) in Concrete Mix Design.
Troubleshooting Recycled Aggregate Concrete
For RCA concrete, give particular attention to:
- water absorption;
- aggregate moisture;
- attached mortar;
- specific gravity;
- source variation.
See Recycled Aggregate Concrete Mix Design.
Daily Concrete Troubleshooting Checklist
When concrete performance changes, check:
- Correct mix-design ID
- Correct mix revision
- Cement source
- SCM source
- Sand source
- Coarse aggregate source
- Aggregate grading
- Sand moisture
- Coarse aggregate moisture
- Batch water
- Admixture dosage
- Admixture product
- Concrete temperature
- Mixing time
- Transportation time
- Plant calibration
- Slump test procedure
- Fresh density
- Segregation
- Bleeding
- Cube preparation
- Curing
- Strength trend
Common Concrete Troubleshooting Mistakes
Adding Water Before Identifying the Cause
Low workability does not automatically mean insufficient design water.
Changing Several Ingredients Together
This makes it impossible to identify which change corrected the problem.
Correcting Plant Error by Changing Mix Design
Plant calibration problems should be repaired at the plant.
Ignoring Aggregate Moisture
Aggregate moisture can affect both:
- batch weight;
- effective free water.
Treating Slump as the Only Quality Check
Also evaluate:
- stability;
- density;
- retention;
- segregation;
- strength.
Assuming More Cement Solves Every Problem
Additional cement can increase:
- cost;
- heat;
- shrinkage;
without correcting the root cause.
Ignoring Temperature and Time
Concrete tested immediately after batching cannot be directly compared with concrete tested after a long hot-weather journey.
Approving a Correction From One Trial
Important changes should be confirmed by repeated trial results before production approval.
Recommended Concrete Mix Troubleshooting Workflow
Identify the Problem
↓
Repeat or Verify the Test
↓
Check Batch Record
↓
Check Aggregate Moisture
↓
Check Batching Plant Calibration
↓
Check Concrete Temperature
↓
Check Material Changes
↓
Review Aggregate Grading
↓
Check Admixture System
↓
Identify Most Likely Root Cause
↓
Change One Main Variable
↓
Repeat Trial
↓
Compare Fresh Concrete Properties
↓
Verify Strength
↓
Conduct Production Verification
↓
Document and Approve Final Adjustment
Frequently Asked Questions
Why Is My Concrete Slump Low Even Though the Design Water Is Correct?
Possible causes include dry aggregate, high concrete temperature, fine aggregate, angular aggregate, insufficient admixture or rapid slump loss.
Should Water Be Added When Concrete Slump Is Low?
Not automatically. First check aggregate moisture, concrete temperature, admixture dosage, grading and transportation time.
Why Does Concrete Segregate?
Segregation may result from excess water, excessive flow, poor grading, inadequate fines, excessive coarse aggregate or improper handling.
Why Does Concrete Bleed?
Bleeding may increase because of excess water, insufficient fines, low paste content or poor aggregate grading.
What Causes a Harsh Concrete Mix?
Common causes include insufficient fine aggregate, excessive coarse aggregate, poor grading, insufficient paste and angular aggregate.
What Causes Sticky Concrete?
Excessive fines, excessive sand, high powder content, low w/cm or excessive viscosity may produce sticky concrete.
Can Concrete Have Good Slump but Poor Pumpability?
Yes. Pumpability also depends on mortar volume, grading, cohesion and slump retention.
Why Does Slump Reduce During Transportation?
High temperature, continued hydration, aggregate absorption and cement–admixture interaction can cause slump loss.
Why Is My 7-Day Concrete Strength Low?
Check SCM content, curing temperature, specimen preparation, actual w/cm, batching and testing before changing the mix.
What Should Be Checked When 28-Day Strength Is Low?
Check actual water, cementitious-material batching, moisture correction, material changes, cube preparation, curing and testing.
Can More Cement Be Added to Correct Low Strength?
Not as the first corrective action. The actual cause should be identified before increasing cementitious content.
Why Do Concrete Cube Strength Results Vary Widely?
Possible causes include variation in water, batching, aggregate moisture, materials, sampling, curing and testing.
Should the Mix Design Be Revised Every Time Slump Changes?
No. Routine production variation should first be investigated and corrected.
Why Is Concrete Suddenly Different Even Though the Mix Design Has Not Changed?
Material source, moisture, temperature, batching accuracy, transportation or admixture conditions may have changed.
What Is the Best Way to Adjust a Trial Mix?
Identify the main problem, change one important variable at a time and document the result.
Related Concrete Mix Design Resources
Concrete Mix Design Procedure as per IS 10262:2019
Water-Cement Ratio in Concrete
Moisture Correction in Concrete Mix Design
Fine and Coarse Aggregate Proportioning
Cement–Admixture Compatibility
Fresh Concrete Density and Yield
Self-Compacting Concrete Mix Design
High-Strength Concrete Mix Design
Manufactured Sand in Concrete Mix Design
Recycled Aggregate Concrete Mix Design
Concrete Mix Design Approval and Production Control
Concrete Batching Plant Calibration
Conclusion
Concrete mix troubleshooting should be based on evidence, not guesswork.
The correct approach is:
Observe → Verify → Identify Root Cause → Make Controlled Adjustment → Re-Test → Document
The most important troubleshooting principles are:
Low Slump ≠ Automatically Add Water
High Slump ≠ Automatically Reduce Admixture
Low Strength ≠ Automatically Add Cement
Segregation ≠ Simply Reduce Slump
Plant Error ≠ Mix-Design Error
One Bad Result ≠ Automatic Mix Redesign
Concrete performance is affected by:
Materials + Moisture + Temperature + Mix Proportions + Admixture + Batching + Mixing + Transportation + Testing
A good mix designer changes the mix only after identifying which part of this system caused the problem.
This systematic approach reduces unnecessary adjustments, improves production consistency and makes each trial useful for developing a reliable final concrete mix.
Engineering Note: Final mix adjustments should comply with the latest applicable requirements of IS 10262, IS 456, relevant material standards, approved project specifications and verified trial-mix results.